


Wooden Cutlery vs. Bamboo Cutlery
Oct 03, 2026
Leave a message
Wooden vs Bamboo Cutlery: 20–30% Moisture Control and Material Selection
Author: [2026-09-15] | By Xiamen Hocso Packaging Products Co., Ltd. Lana Zheng zhenglanlan@hocso.com
For disposable cutlery, bamboo and wood behave differently because their fiber structure, density, moisture absorption and machining characteristics are not identical. Bamboo can provide a favorable strength-to-weight ratio, while wood offers a wider range of species, hardness and surface characteristics; the final cost and durability depend heavily on raw-material grade, moisture content, machining yield, packaging and storage conditions.
For wholesale buyers, comparing the material price alone is insufficient. The relevant purchasing variables are raw-material yield, finished-piece weight, moisture content, dimensional tolerance, surface defects, mold control, carton CBM and breakage during transportation.
1. Bamboo vs Wood Hardness: 0.4–1.0% Moisture Target Control
1.1 Hardness Depends on Species, Density and Fiber Direction
There is no single hardness value for "wood" or "bamboo."
Wood may range from relatively soft species to very hard hardwoods. Bamboo also varies significantly by species, maturity, culm position and processing method.
For disposable cutlery, hardness is only one parameter. Flexural strength, impact resistance, grain orientation, fracture behavior and surface integrity can have a greater effect on the user's experience.
| Property | Bamboo | Wood |
|---|---|---|
| Biological structure | Grass with longitudinal vascular bundles | Secondary xylem with annual growth structure in many species |
| Fiber orientation | Strongly longitudinal | Species-dependent grain structure |
| Density | Species and culm-position dependent | Wide range by species |
| Hardness | Generally moderate to high for many commercial bamboo grades | Highly species-dependent |
| Strength-to-weight ratio | Often favorable | Depends strongly on species |
| Grain direction | Predominantly longitudinal | Straight, interlocked or irregular depending on species |
| Moisture response | Swelling/shrinkage with moisture changes | Swelling/shrinkage with moisture changes |
| Surface machining | Requires controlled cutting and sanding | Generally established woodworking process |
| Food-contact surface | Must be smooth and free of splinters | Must be smooth and free of splinters |
| Disposable cutlery suitability | Forks, knives, spoons, sporks and picks | Forks, knives, spoons and stirrers |
The important point for procurement is that a specification such as "bamboo is harder than wood" is too broad to use as a quality requirement.
A factory should instead define:
- Material species or grade.
- Raw-material moisture content.
- Finished-piece moisture content.
- Product weight.
- Dimensional tolerance.
- Bending or breakage requirement.
- Surface-defect limit.
- Splinter acceptance criteria.
1.2 Moisture Content Controls Dimensional Stability
Both bamboo and wood are hygroscopic materials. They exchange moisture with surrounding air until reaching an equilibrium moisture condition.
During international transportation, this matters because a product manufactured in a humid environment may experience a different equilibrium condition after shipment to a dry warehouse.
Changes in moisture content can cause:
- Dimensional shrinkage.
- Dimensional expansion.
- Warping.
- Surface cracking.
- Increased microbial growth risk under favorable conditions.
- Changes in package weight.
- Increased breakage during handling.
A production specification should therefore define moisture content rather than simply stating "dry bamboo" or "dry wood."
1.3 Moisture-Control Specification for Disposable Cutlery
| Control Point | Procurement Requirement |
|---|---|
| Incoming raw material | Moisture inspection by batch |
| Production environment | Record temperature and relative humidity |
| Finished cutlery | Measure moisture content before packing |
| Storage | Dry, ventilated warehouse |
| Carton storage | Keep cartons off the floor |
| Container loading | Avoid loading visibly wet cartons |
| Long-distance shipping | Use moisture-control packaging where required |
| Inspection | Record batch number and moisture result |
A single moisture value should not be treated as universal for every species and destination climate. The factory and buyer should establish an acceptable range through sample testing and storage validation.
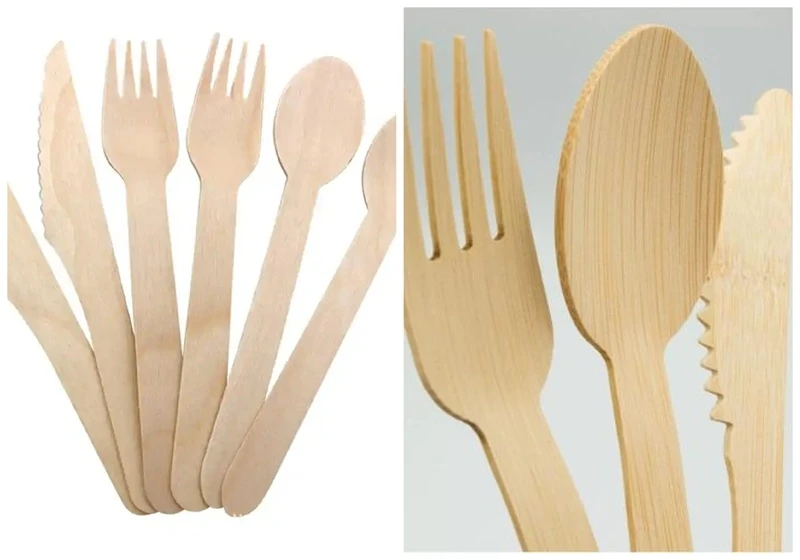
2. Bamboo vs Wood Moisture Resistance: 60–80% RH Storage Control
2.1 Neither Material Is Naturally Moisture-Proof
Bamboo and wood are both porous, hygroscopic materials.
Their performance changes according to:
- Relative humidity.
- Temperature.
- Storage duration.
- Initial moisture content.
- Packaging permeability.
- Surface treatment.
- Container ventilation.
- Warehouse conditions.
For disposable foodservice products, "water-resistant" should therefore not be interpreted as "waterproof."
A bamboo fork used for several minutes with a moist meal is a different application from a bamboo spoon stored for six months inside a humid warehouse.
2.2 Water Contact and Short-Term Food Use
The buyer should test the finished utensil with the actual food conditions.
For example, a supplier qualification test can include:
| Test Condition | Example Test Parameter |
|---|---|
| Food temperature | 25°C / 60°C / 80°C |
| Contact duration | 5 / 15 / 30 minutes |
| High-moisture food | Rice, noodles, salad, fruit |
| High-fat food | Fried or oily food |
| Surface evaluation | Cracking, fuzzing, delamination |
| Mechanical evaluation | Bending and breakage |
| Sensory evaluation | Odor, taste and surface feel |
The purpose is not to assign one universal "water-resistance rating." It is to determine whether the finished product remains fit for its intended service period.
2.3 Bamboo and Wood in High-Humidity Warehouses
Warehouse conditions can have a larger effect on mold risk than the original material choice.
A pallet stored in a poorly ventilated warehouse at high relative humidity can experience very different conditions from the same pallet stored in a dry, temperature-controlled facility.
For this reason, a factory quality system should monitor:
- Relative humidity.
- Temperature.
- Warehouse ventilation.
- Carton condition.
- Pallet clearance from the floor.
- Storage duration.
- Product moisture content.
- Incoming and outgoing batch records.
Request Bamboo Cutlery Samples
3. Bamboo vs Wood Processing: 4 Core Manufacturing Stages
The manufacturing route directly affects cost, dimensional consistency and finished-product yield.
Although both materials require cutting, shaping and sanding, bamboo and wood have different raw-material structures.
3.1 Raw-Material Preparation
Bamboo is typically harvested as a hollow culm and then processed into strips, sections or blanks suitable for further machining.
Wood is normally supplied as logs, boards, blocks or pre-cut blanks depending on the manufacturing system.
The raw-material preparation stage affects material utilization.
| Manufacturing Factor | Bamboo | Wood |
|---|---|---|
| Raw form | Culm / strip / laminated blank | Log / board / block / blank |
| Main challenge | Culm geometry and fiber orientation | Species, grain and defect distribution |
| Yield control | Strip selection and cutting pattern | Board layout and defect removal |
| Moisture control | Required | Required |
| Defect screening | Knots, cracks, discoloration | Knots, cracks, resin pockets, discoloration |
| Production consistency | Depends on culm selection | Depends on species and grade |
3.2 Cutting and Blanking
Cutting converts the raw material into blanks close to the final utensil geometry.
For bamboo, cutting direction matters because the material has strong longitudinal fiber orientation.
For wood, grain direction and local defects influence the cutting result.
Poor cutting can create:
- Fiber tearing.
- Edge cracking.
- Uneven surfaces.
- Short grain sections.
- Excessive machining allowance.
- Higher material waste.
3.3 Hot Pressing and Forming at Controlled Temperature
Certain bamboo and wood cutlery products require hot pressing or forming to obtain a defined spoon bowl, fork geometry or curved profile.
The forming process must control:
- Temperature.
- Pressure.
- Dwell time.
- Mold geometry.
- Material moisture.
- Cooling conditions.
Excessive forming stress can cause cracking or spring-back. Insufficient forming can produce dimensional variation.
For mass production, mold repeatability is important because even a small change in bowl depth or handle curvature can affect packing and user experience.
3.4 Grinding and Polishing
Grinding removes rough fibers and machining marks.
For food-contact disposable cutlery, the surface should be checked for:
- Splinters.
- Sharp edges.
- Rough fiber ends.
- Burrs.
- Cracks.
- Uneven sanding.
- Surface contamination.
A product can meet dimensional requirements and still fail a practical foodservice inspection because of poor surface finishing.
4. Manufacturing Cost: 0.5 g Weight Variation Can Affect Material Spend
4.1 Raw Material Is Only One Part of Unit Cost
The actual cost of a disposable bamboo or wooden utensil includes:
Raw material + material loss + machining + sanding + forming + labor + quality inspection + packaging + warehouse + freight + rejected pieces.
For high-volume procurement, product weight is particularly important.
If one utensil weighs 5.0 g, one million pieces represent approximately:
5,000 kg of finished product.
If the approved design is changed from 5.0 g to 5.5 g, the finished-material requirement increases by approximately:
500 kg per million pieces, before considering production loss.
That difference can affect both material cost and freight.
4.2 Yield Is a Manufacturing Cost Variable
A low-cost raw material is not necessarily a low-cost finished utensil if the usable yield is poor.
| Cost Factor | Procurement Question |
|---|---|
| Raw material price | What is the price per kg or m³? |
| Material yield | What percentage becomes finished products? |
| Product weight | How many grams per piece? |
| Reject rate | What percentage is rejected? |
| Processing time | How many pieces per production hour? |
| Sanding loss | How much material is removed? |
| Packaging | Pieces per inner pack and carton? |
| Carton CBM | How much volume per 10,000 pieces? |
| Freight | What is the delivered cost per 1,000 pieces? |
This is why a supplier comparison should use cost per 1,000 delivered pieces, not only raw-material price.
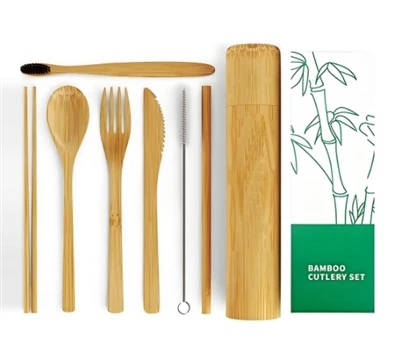
5. Bamboo vs Wood Durability: 5 Mechanical Tests for Production Approval
A disposable utensil does not need the same mechanical properties as reusable stainless steel cutlery. It needs enough strength for the intended food and service period.
The correct approach is therefore application-specific mechanical testing.
5.1 Bending Test
A fork or spork should tolerate normal hand force without excessive permanent deformation.
The test should define:
- Loading direction.
- Support distance.
- Applied force.
- Loading rate.
- Deflection limit.
- Failure mode.
5.2 Tine Breakage Test
Fork and spork tines are high-risk areas because they have small cross-sections.
Inspection should look for:
- Tine cracking.
- Tine fracture.
- Fiber splitting.
- Uneven tine length.
- Sharp fracture surfaces.
5.3 Bowl Load Test
For spoons and sporks, the bowl should resist deformation during normal scooping.
The test should use a defined load and support condition rather than an informal hand test.
5.4 Handle Flex Test
Handle thickness, fiber direction and product geometry all influence flexural behavior.
A production specification should define an acceptable deformation or failure criterion.
5.5 Drop and Transport Simulation
Packaging should be evaluated together with the utensil.
| Test | Typical Evaluation |
|---|---|
| Individual bending | Cracking / permanent deformation |
| Tine loading | Breakage / splitting |
| Bowl loading | Permanent deformation |
| Handle flexing | Cracking / fracture |
| Carton drop | Broken pieces / package damage |
| Vibration | Product abrasion / breakage |
| Compression | Carton deformation |
| Humidity exposure | Mold / discoloration / dimensional change |
Exact test conditions should be established according to product geometry, packaging and transportation mode.
6. Mold Risk During 30–180 Day Storage: Moisture, Ventilation and Packaging
Mold should not be described as a fixed percentage for bamboo or wood because the risk depends on multiple environmental variables.
The relevant variables include:
- Product moisture content.
- Relative humidity.
- Temperature.
- Storage duration.
- Air circulation.
- Packaging permeability.
- Initial microbial load.
- Surface contamination.
- Warehouse hygiene.
A claim such as "bamboo has a 2% mold rate" is not technically meaningful unless the test defines the population, environment, storage period and acceptance criteria.
6.1 A Practical Mold-Risk Validation Program
A factory can establish a controlled storage test using defined environmental conditions.
| Test Variable | Example Setting |
|---|---|
| Storage duration | 30 / 60 / 90 / 180 days |
| Temperature | 25–30°C |
| Relative humidity | 60% / 75% / 85% RH |
| Sample quantity | Defined by batch |
| Packaging | Actual export packaging |
| Inspection interval | 7–30 days |
| Inspection items | Mold, odor, discoloration, surface change |
| Moisture measurement | Before and after storage |
| Result | Pass / fail according to agreed specification |
This type of test provides more useful procurement information than a generic statement about bamboo or wood.
6.2 Cross-Contamination Prevention
Mold prevention starts before the finished product enters the warehouse.
Production areas should control:
- Raw-material segregation.
- Clean and dirty material flow.
- Pallet hygiene.
- Finished-product handling.
- Packaging cleanliness.
- Employee handling practices.
- Carton storage.
- Water exposure.
For food-contact disposable products, cross-contamination prevention should be treated as part of production control rather than only a final inspection activity.
7. International Shipping Loss: 1–5% Damage Must Be Measured, Not Assumed
Transportation damage is influenced by packaging design, carton compression, stacking height, pallet configuration, container handling and product geometry.
A fragile wooden fork packed with insufficient internal protection may experience a different breakage rate from a thicker bamboo fork packed in a tightly controlled carton.
Therefore, buyers should measure transportation performance using the actual export package.
7.1 Carton Compression and Drop Testing
A transport-validation program can include:
- Carton drop test.
- Compression test.
- Vibration simulation.
- Pallet stacking test.
- Container loading review.
- Humidity exposure.
- Post-transport product inspection.
The objective is to identify the damage rate per shipment, not simply to test whether one carton survives a manual drop.
7.2 Shipping Loss and Carton CBM
For lightweight disposable tableware, freight cost is frequently driven by volume rather than product weight.
A useful procurement metric is:
Pieces per CBM = Total pieces ÷ Total carton volume
Another is:
Delivered cost per 1,000 pieces = Product cost + Packaging cost + Freight + Insurance + Import-related costs
| Shipping Parameter | Why It Matters |
|---|---|
| Pieces/carton | Determines packing density |
| Carton dimensions | Determines CBM |
| Carton gross weight | Affects handling and freight |
| Cartons/pallet | Determines warehouse efficiency |
| Pieces/pallet | Useful for distribution planning |
| Container utilization | Determines freight efficiency |
| Breakage rate | Direct product loss |
| Moisture exposure | Mold and dimensional risk |
| Packaging material | Protects against abrasion and impact |
8. Bamboo vs Wood for Wholesale: 10 Procurement Parameters
For a restaurant group, distributor or importer, a material decision should be based on the complete supply chain.
8.1 Material and Engineering Parameters
- Material species or grade: Identify the actual material.
- Moisture content: Define the acceptable production range.
- Product weight: Lock the approved gram weight.
- Dimensions: Define length, width and thickness.
- Mechanical performance: Specify bending and breakage requirements.
- Surface quality: Define splinter and roughness limits.
- Food-contact compliance: Obtain documents applicable to the destination market.
- Packaging format: Bulk, individual wrapping or meal set.
- Carton CBM: Calculate shipping volume.
- Storage validation: Test the actual packaging under expected warehouse conditions.
8.2 Bamboo and Wood Cost Matrix
| Procurement Factor | Bamboo | Wood |
|---|---|---|
| Raw-material variability | Species and culm position dependent | Species and grade dependent |
| Weight control | Good with controlled blanks | Good with controlled blanks |
| Strength-to-weight potential | Often favorable | Highly species-dependent |
| Machining | Requires fiber-direction control | Mature woodworking process |
| Surface finishing | Sanding required | Sanding required |
| Moisture sensitivity | Yes | Yes |
| Mold risk | Environment-dependent | Environment-dependent |
| Packaging sensitivity | Medium to high | Medium to high |
| Freight sensitivity | Volume and weight dependent | Volume and weight dependent |
| Sustainability claim | Must be supported by material documentation | Must be supported by material documentation |
Neither material should be approved solely because it is marketed as "natural" or "eco-friendly."
Button Text: Compare Wholesale Cutlery Options
9. Food-Contact and Sustainability Documentation: EN 13432, ASTM D6400 and FDA CFR 21
Wood and bamboo are natural materials, but "natural" does not automatically mean compliant with every food-contact or environmental requirement.
Documentation should match the destination market and the exact finished product.
9.1 Food-Contact Documentation
Depending on the destination market and product configuration, buyers may request documentation covering:
- Raw-material composition.
- Food-contact suitability.
- Heavy-metal limits where applicable.
- Chemical migration requirements.
- Coatings or adhesives.
- Printing inks.
- Packaging materials.
For the United States, food-contact compliance may involve applicable FDA 21 CFR requirements.
European buyers may require documentation under applicable EU food-contact legislation.
The exact regulatory route should be confirmed according to the finished product, additives, coatings, inks and intended food-contact conditions.
9.2 Compostability Claims
Wood and untreated bamboo are not equivalent to certified compostable polymer products.
For any compostability claim, the buyer should ask:
| Document | Procurement Question |
|---|---|
| Material declaration | What is the actual composition? |
| Finished-product test | Was the actual utensil tested? |
| EN 13432 | Does the certification apply to the finished product? |
| ASTM D6400 | Does the product fall within the applicable certification scope? |
| BPI certification | Is the exact product certified? |
| Packaging declaration | Is the packaging compatible with the stated disposal claim? |
| Coating declaration | Does coating change the end-of-life claim? |
A supplier should not use a raw-material certificate as proof that every finished utensil automatically meets a compostability requirement.
10. China Wooden Utensils Manufacturer: Factory Audit at 6 Production Controls
A wooden utensils manufacturer should be evaluated by production controls rather than catalog photographs.
For a China supplier or factory, buyers should review:
10.1 Raw-Material Traceability
The factory should be able to identify the material source, grade and incoming batch.
10.2 Moisture Control
Moisture should be measured rather than judged visually.
10.3 Machining Consistency
Cutting, forming and sanding should produce repeatable dimensions.
10.4 Surface Inspection
The inspection process should identify splinters, cracks, sharp edges and contamination.
10.5 Packaging Control
The approved packaging specification should define pieces per bag, bags per carton, carton dimensions and carton strength.
10.6 Final Inspection
AQL sampling can be incorporated into the purchase specification. AQL 2.5 may be used as an agreed sampling parameter for selected major defects, but it should not be treated as a universal legal requirement.
For food-contact products, critical defects and contamination risks should have separate acceptance criteria.
11. HOCSO Disposable Bamboo and Wooden Cutlery: 10,000–350 Million Piece Planning
Xiamen Hocso Packaging Products Co., Ltd. was established in 2014 in Xiamen, Fujian, China and focuses on disposable foodservice products including bamboo and wooden cutlery, disposable cutlery sets, chopsticks, napkins and toothpicks.
The company reports more than 200 employees, approximately 10,000 m² of production space and production capacity of about 1 million disposable cutlery sets per day, equivalent to approximately 350 million sets annually at the stated production level.
For wholesale buyers, the useful evaluation points are production capacity, material control, product consistency, packaging capability, quality inspection and export logistics.
A factory qualification should still be based on the buyer's approved specification and sample-production results.
11.1 Recommended Factory Approval Data
| Item | Required Approval Data |
|---|---|
| Material | Bamboo / wood species or grade |
| Moisture | Agreed specification |
| Weight | g/piece |
| Dimensions | mm |
| Surface | Splinter and defect criteria |
| Mechanical test | Agreed load and failure criteria |
| Packaging | Pieces/bag and pieces/carton |
| Carton | L × W × H |
| CBM | m³/carton |
| Inspection | Sampling level and defect classification |
| Compliance | Destination-market documentation |
| Production | MOQ and lead time |
| Shipment | Loading plan and estimated container utilization |
12. Bamboo vs Wood Selection: 8 Engineering Questions Before Mass Production
Before issuing a purchase order, the buyer should answer:
- What exact bamboo or wood grade is being supplied?
- What moisture-content range is accepted at final packing?
- What is the approved weight per piece?
- What dimensional tolerance applies?
- What bending and breakage criteria apply?
- What storage humidity and temperature are expected?
- What packaging configuration protects the product during ocean freight?
- What food-contact and environmental documents are required in the destination market?
These eight questions convert a generic "eco cutlery" purchase into a measurable manufacturing specification.
13. Wooden vs Bamboo Cutlery: Cost, Durability and Logistics Summary
| Decision Factor | Bamboo | Wood |
|---|---|---|
| Raw-material consistency | Depends on bamboo grade and culm selection | Depends strongly on species and grade |
| Mechanical performance | Generally good when fiber direction is controlled | Highly variable by species and grain |
| Moisture sensitivity | Requires controlled storage | Requires controlled storage |
| Mold control | Dependent on moisture and warehouse environment | Dependent on moisture and warehouse environment |
| Processing | Cutting, forming and sanding | Cutting, forming and sanding |
| Material yield | Strongly affected by blank geometry | Strongly affected by board/block quality |
| Product weight | Must be controlled by design | Must be controlled by design |
| Surface finish | Requires splinter control | Requires splinter control |
| Shipping damage | Packaging-dependent | Packaging-dependent |
| Sustainability documentation | Material and treatment dependent | Material and treatment dependent |
| Best purchasing metric | Delivered cost + performance | Delivered cost + performance |
The correct comparison is therefore not simply "bamboo is cheaper" or "wood is stronger."
The engineering question is:
Which material and production specification delivers the required mechanical performance, storage stability and delivered cost for the intended foodservice application?
14. Final Procurement Specification: 12 Data Points for Wholesale Bamboo Cutlery
For a wholesale bamboo cutlery program, the purchase specification should contain measurable data rather than broad material descriptions.
A practical specification can include:
- Material and grade.
- Raw-material moisture range.
- Finished-product moisture range.
- Product length.
- Product width.
- Product thickness.
- Weight per piece.
- Mechanical test requirement.
- Surface-defect acceptance criteria.
- Packaging configuration.
- Carton CBM and gross weight.
- Food-contact and destination-market documentation.
For large restaurant, airline catering or distributor programs, the factory should also provide samples from production rather than approving a product from photographs alone.
HOCSO can supply bamboo disposable cutlery and wooden disposable cutlery in different formats and packing configurations for foodservice procurement. Buyers can compare material, dimensions, packaging, MOQ and destination-market documentation before production approval.
FAQ: Bamboo and Wooden Cutlery Manufacturing
What is more durable for wholesale disposable cutlery, bamboo or wood?
Durability depends on species, density, fiber direction, moisture content, thickness and product geometry. Bamboo can provide a favorable strength-to-weight ratio, but the finished utensil should be approved through bending, tine-breakage and surface tests.
How should buyers control mold risk when importing bamboo or wooden cutlery from China?
Specify finished-product moisture limits, dry storage, carton protection and warehouse humidity controls. Validate the actual export package under 30-, 60-, 90- or 180-day storage conditions instead of relying on a generic mold-rate claim.
What information should a wooden utensils manufacturer provide before mass production?
Request material grade, moisture specification, piece weight, dimensions, mechanical test results, food-contact documents, packaging details, carton CBM, MOQ, production lead time and an agreed final inspection plan.
Request Disposable Cutlery Samples
Send Inquiry